When a hardware startup is burning through its seed round, every line item on the budget becomes a negotiation. Manufacturing costs are among the first places early-stage teams look to cut. A lower quote from an unfamiliar machine shop feels like smart financial management. It often looks reasonable on paper, and the savings appear immediate and concrete. The problems that follow are neither immediate nor obvious — they accumulate quietly until they aren’t quiet at all.
This pattern repeats across industries, from consumer electronics to industrial equipment to medical device prototyping. Startups that prioritize unit cost over process quality during early production runs frequently discover that what they saved in machining fees gets spent several times over in rework, delayed timelines, failed audits, and damaged supplier relationships. Understanding why this happens requires looking honestly at what gets compressed when machining costs are driven down artificially.
What “Cheap” Actually Compresses in a Machining Operation
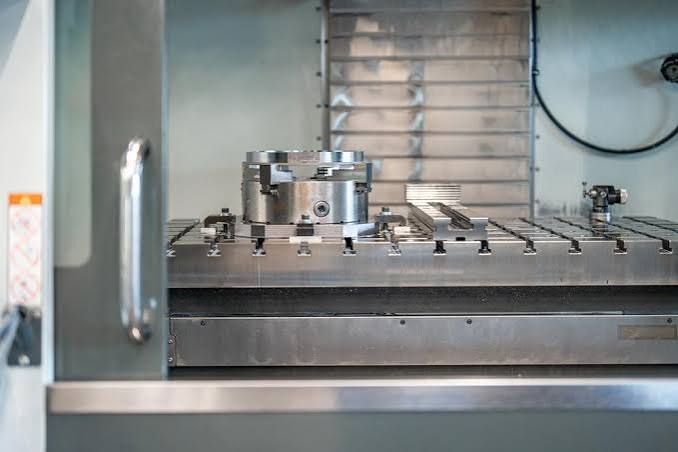
The economics of cnc metal machining are more fixed than most buyers assume. A shop running tight margins on a low-ball quote has limited options for where those savings come from. Tooling quality, machine calibration schedules, operator experience, and in-process inspection are all cost centers. When a shop accepts a job at a price that doesn’t support those investments, something gives. The question is only which element gets reduced and how visible that reduction becomes before parts reach the customer.
Buyers who understand how machining operations are structured — setup time, programming, tooling wear, cycle time, and inspection — can evaluate quotes more accurately. A price that sits significantly below market rate for a given part complexity is not a discount. It is a signal that one or more of those cost centers has been deprioritized. For startup founders focused on prototype validation or first production runs, this matters in ways that go well beyond the immediate order.
Tooling and Process Consistency
Tooling is a significant and recurring cost in any machining environment. Cutting tools wear, and worn tools produce parts that drift from specification. A shop managing costs aggressively will run tooling longer than recommended, introducing gradual dimensional variation that may not appear in every part but surfaces unpredictably across a batch. For a startup receiving a hundred parts, this might mean ten that pass inspection and ninety that require secondary review — or the reverse, with problems only discovered after assembly.
Process consistency depends on documented procedures, tool change schedules, and calibrated measurement equipment. These are not visible to the buyer during quoting. They are visible only in the output over time. Startups that work with a single machining partner across multiple orders often discover inconsistency between batches — not because the shop changed, but because no structured process existed to prevent variation in the first place.
Operator Experience and Setup Quality
Programming a CNC machine for a new part requires experienced judgment, not just technical ability. An experienced machinist anticipates where a part design creates fixturing challenges, where tool paths may generate excessive heat, or where a particular material behaves unpredictably during cutting. Shops competing aggressively on price often operate with a higher proportion of junior operators or rely on automated programming without sufficient manual review.
The consequences tend to show up in edge cases — parts with thin walls, tight tolerances in specific areas, or features that require sequential setups. These are exactly the kinds of parts that early-stage hardware products often require, because startups are frequently building something that doesn’t have an off-the-shelf equivalent. The complexity of the part and the experience gap in the shop create a mismatch that a low quote does not account for.
Why Startups Are Particularly Exposed to This Risk
Established manufacturers have quality teams, incoming inspection protocols, and supplier scorecards. They have seen what poor machining quality costs them in real terms and have built systems to identify and reject it before it enters their production line. Startups typically have none of these structures. A founder or engineer receiving a batch of machined parts may have the domain knowledge to evaluate the design but not the metrology background to catch dimensional issues that fall just outside tolerance.
This exposure compounds when the parts feed directly into a prototype that needs to demonstrate function for investors, customers, or regulatory reviewers. A part that looks correct but performs inconsistently can delay a product launch by weeks or months. It can compromise a customer demonstration that took months to arrange. It can introduce doubt into an engineering validation process that was already tight on time. None of these costs appear in the original quote comparison.
The Rework Cycle and Its True Cost
Rework is the most immediate and visible consequence of poor machining quality. A batch of parts arrives, some percentage fails inspection or fails in function, and the startup now faces a decision: return the parts for correction, source from a different supplier, or attempt internal remediation. Each of these paths carries costs that extend beyond the financial. Returning parts consumes time, strains the supplier relationship, and delays downstream processes. Finding a new supplier mid-project resets the learning curve on the part’s requirements. Internal remediation, where possible at all, consumes engineering hours that were allocated elsewhere.
The rework cycle is also rarely a single event. Startups that accept a marginally acceptable batch to meet a deadline often find that the next batch carries the same problems. Without a clear quality requirement communicated and enforced from the start, a low-cost supplier has no incentive to improve. The relationship stabilizes at a level of quality that the startup has implicitly accepted by continuing to place orders.
Regulatory and Certification Implications
For startups in sectors where components must meet safety or performance standards — whether industrial, medical, or aerospace-adjacent — machining quality connects directly to regulatory standing. Parts produced without documented process controls or traceable inspection records may not support the certification paperwork that regulators require. The National Institute of Standards and Technology’s Manufacturing Extension Partnership has consistently noted that quality system gaps in early manufacturing stages create downstream compliance risks that are expensive to remediate after the fact.
A startup that discovers its machining partner cannot produce conforming inspection documentation may find itself rebuilding an entire production history for audit purposes. This situation is more common than it appears, and it almost always traces back to initial supplier selection driven primarily by unit cost.
How Experienced Buyers Evaluate Machining Partners Differently
Buyers with direct manufacturing experience approach supplier selection with a different framework. Price is relevant, but it enters the conversation after capability, quality systems, and communication have been evaluated. A capable shop that quotes at a fair market rate for the work involved is a better long-term partner than a low-cost shop that requires constant monitoring and remediation.
The questions that experienced buyers ask early are revealing. They ask about the shop’s inspection equipment and calibration schedule. They ask how the shop handles a part that goes out of tolerance mid-run. They ask about the machinist’s background with the specific material or feature type. These questions are not adversarial. They establish whether the shop’s internal processes are structured enough to produce consistent output without the buyer managing every detail.
First Article Inspection as a Baseline Expectation
One of the clearest indicators of a quality-oriented machining operation is how it handles first article inspection. Before running a full batch, a competent shop will produce a single part, measure it comprehensively, and confirm that the process is capable of holding the required tolerances before committing to volume. Some shops include this as standard practice. Others treat it as an optional upsell. The difference matters significantly for startups placing their first production orders.
A shop that resists first article inspection on the basis of cost or timeline is a shop that is not positioned to catch systematic errors before they affect an entire batch. For a startup with limited budget and no tolerance for wholesale batch failures, this resistance is a meaningful warning signal.
The Long-Term Relationship Cost That Startups Underestimate
Manufacturing relationships improve over time when both parties invest in them. A machining partner that understands a startup’s parts, tolerances, and production rhythm develops efficiency that a new supplier cannot match. This accumulated knowledge has real value — it reduces setup time, reduces error rates, and allows the shop to flag potential design issues before they become production problems.
Startups that chase the lowest quote on every order forfeit this value entirely. They reset the learning curve repeatedly, manage more variation across batches, and lose the informal communication that comes from a developed working relationship. The cumulative cost of that instability often exceeds the savings that motivated the constant switching.
Closing Perspective
The case for prioritizing quality in machining partnerships is not an argument against cost discipline. Startups operate under genuine financial constraints, and those constraints are real. The argument is for accuracy in how costs are evaluated. A machining quote is not a complete picture of what a production batch will cost. It is the starting point. The rest of the cost — rework, delays, failed inspections, remediation, and lost time — accumulates downstream, often in ways that are difficult to attribute directly to the original sourcing decision by the time they appear.
Startups that learn this early, usually from a single painful experience, tend to adjust their supplier evaluation process permanently. Those that learn it late — after a product launch has been delayed or a customer relationship has been strained — pay a higher price for the same lesson. The discipline of evaluating machining partners on capability and process quality rather than unit cost alone is not a luxury reserved for companies with large procurement teams. It is a basic form of operational risk management that any hardware-focused startup can apply, regardless of stage or budget.