Packaging failure rarely announces itself in advance. A box that looked fine during a sample review collapses under transit pressure. A closure that held during initial testing begins to release under humidity. A flap designed to tuck securely starts to pop open on the retail shelf. These are not unusual problems. They are predictable outcomes when the structural logic behind a package has not been properly thought through from the beginning.
For product managers, packaging engineers, and procurement leads who deal with folding carton formats, the tuck box is one of the most commonly specified enclosures across a wide range of industries. It is also one of the most misunderstood. Its apparent simplicity — a folding sleeve with tucked flaps at either end — creates the false impression that it requires minimal engineering attention. In practice, the difference between a tuck box that performs reliably and one that causes downstream problems comes down to a series of structural decisions that must be made deliberately, not assumed.
This article examines those decisions in order, from the underlying principles of the format to the specific variables that determine whether a tuck box holds up in the real world.
What a Tuck Box Actually Is and Why the Format Is More Nuanced Than It Looks
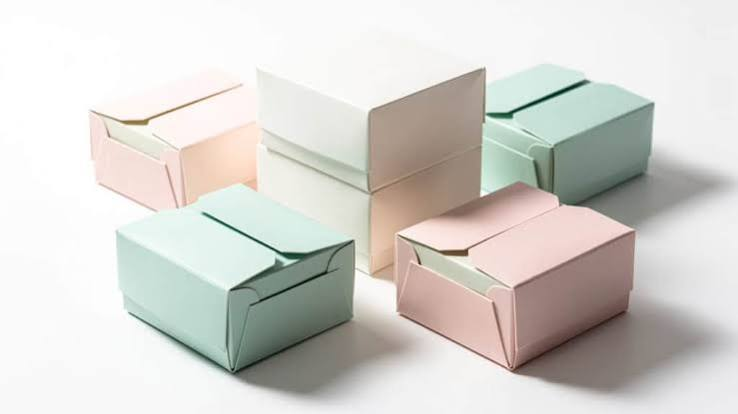
A tuck box is a folded carton format in which the end closures are formed by folded flaps that insert into the interior of the box rather than being glued shut. The basic configuration involves a main body panel, two side panels, and end flaps that lock or tuck into place. This makes it a reclosable format by design, which is part of its commercial appeal — particularly in retail, pharmaceutical, cosmetics, and consumer electronics applications where the end user may need to access and reseal the package more than once.
The format varies significantly depending on how the tuck ends are engineered. A straight tuck box uses flaps that tuck in the same direction on both ends. A reverse tuck configuration staggers the direction of the flap openings, which improves structural resistance when the box is under side pressure. Neither version is universally superior. The right choice depends on the product weight, the filling method used in production, the orientation of the box during transit, and the expected handling conditions before it reaches the end user.
Understanding this from the outset matters because many packaging specifications are written based on visual reference alone. A buyer selects a tuck style because it resembles a package they have seen, not because the structural logic has been evaluated against their specific product and supply chain requirements. That gap between appearance and function is where most tuck box failures begin.
The Role of the Tuck Flap in Load Distribution
The tuck flap is the most mechanically active part of this format. It serves as both the closure mechanism and a partial structural contributor to the rigidity of the end panel. When a tuck flap is too short, the engagement depth inside the box is insufficient to hold the closure under any real lateral pressure. When it is too long, it may buckle during insertion, which can cause cosmetic damage to the box interior or slow down automated filling lines.
The flap also distributes compressive load. When boxes are stacked, as they almost always are during shipping, the end panels bear a meaningful portion of the vertical force traveling through the stack. A flap that does not sit flush with the interior walls creates a gap that reduces the effective stiffness of the end panel. That gap, invisible from the outside, is what causes a stack of boxes to begin collapsing inward under sustained pressure.
Grain Direction and Its Effect on Fold Quality
Paperboard, like all fiber-based materials, has a grain direction determined by the orientation of the fibers during the manufacturing process. According to the Technical Association of the Pulp and Paper Industry, grain direction directly affects how board behaves under bending stress. A fold made parallel to the grain will be cleaner, sharper, and more resistant to cracking. A fold made against the grain tends to crack the surface layer of the board, which weakens the fold line and creates visible damage that accelerates structural fatigue over time.
In tuck box production, grain direction must be aligned so that the primary fold lines — those forming the main body of the box — run parallel to the grain. This is not always possible for every fold line on a complex blank, but priority should be given to the folds that carry the most repeated stress. For a tuck box, those are the corner scores and the flap fold lines at each end. When grain alignment is ignored or treated as a secondary concern during die design, the result is a box that cracks, warps, or loses its shape after minimal handling.
Score Lines, Creases, and the Precision Required to Make Them Work
Every fold in a tuck box is preceded by a score line — a compressed channel in the paperboard that guides the fold and reduces resistance at the bending point. The quality of that score determines whether the box folds cleanly, whether the panels align correctly, and whether the box retains its rectangular geometry after assembly. Score lines that are too shallow require excessive force to fold and tend to crack the surface. Score lines that are too deep weaken the board and create hinge points that fail under repeated use.
The scoring process is part of the die-cutting operation, which means the precision of the die itself directly controls the quality of every score on every blank produced. A worn or poorly maintained die delivers inconsistent score depths across a production run, which creates variation in fold quality that may not become visible until the boxes are assembled and filled. By that point, the problem is embedded in completed inventory.
Why Consistency Across a Production Run Matters More Than a Single Sample
Packaging decisions are often made based on pre-production samples, which represent the best output of a tooling setup rather than the average output of a sustained production run. A die that produces excellent samples at the start of a run may deliver degraded results after extended use if it has not been maintained or if the cutting edges have worn unevenly.
For tuck boxes specifically, the critical tolerance points are the tuck flap length, the width of the score channels, and the registration between cuts and scores. If any of these shift outside an acceptable range during a long production run, the resulting blanks will fold inconsistently, close improperly, or fail to run cleanly through automated filling equipment. The cost of that inconsistency is not absorbed at the packaging stage. It is absorbed downstream, in production delays, rejected product, or customer complaints.
Material Selection as a Structural Decision, Not Just a Cost Variable
The paperboard specified for a tuck box determines its functional ceiling. No amount of precision in die design or folding can compensate for a substrate that lacks the stiffness, caliper, or surface integrity required for the application. Boards vary significantly in how they perform under compression, how they respond to moisture, and how cleanly they accept a score and fold.
Solid bleached sulfate board is commonly used in pharmaceutical and cosmetics applications because it offers consistent caliper and a clean surface for printing. Coated unbleached kraft provides better compression strength and is often preferred when transit durability is the primary concern. Recycled-content boards offer cost advantages but can introduce variability in thickness and surface quality that affects fold precision. None of these choices is inherently wrong. Each involves a set of trade-offs that must be evaluated against the demands of the specific product, fill process, and distribution environment.
How Moisture Affects Structural Integrity Over Time
Paperboard responds to changes in ambient humidity. In high-humidity environments, board absorbs moisture from the air and loses stiffness. Score lines soften. Tuck flaps lose their spring and fail to hold tension against the interior walls. Panels that were flat during production develop a slight bow that causes the box to resist closing properly or causes the tuck closure to release under minimal pressure.
This is a particular concern for products distributed across climate zones or stored in warehouses without full climate control. Coating selection, board composition, and the addition of moisture-resistant treatments are all variables that can be used to extend performance in difficult conditions. These are decisions made at the specification stage, not after the product is in distribution.
How Die Design Ties All of These Variables Together
The die is the single tool that translates a flat board specification into a functional blank. It cuts the outer contour of the blank, creates the score lines that define the folds, and in some cases punches any windows, vents, or registration holes required by the design. The quality of the die and the precision with which it is maintained determine whether all of the structural decisions made upstream — board selection, grain direction, score depth, flap geometry — are actually realized in the finished blank.
A well-designed die accounts for material behavior, not just geometry. It compensates for the spring-back that occurs when paperboard is scored. It positions cuts and scores to work with the grain direction of the board. It allows for the tight tolerances needed to keep tuck flaps functional across a full production run. A die that is designed with only the geometry of the finished box in mind, without accounting for how the material will behave during cutting and folding, produces results that look correct on paper and fail in production.
Closing Thoughts
A tuck box is not a complicated package by the standards of modern packaging engineering. But its simplicity is deceptive. The format works well when every structural variable has been treated as a real decision — material selection, grain alignment, score depth, flap geometry, and die precision — and when those decisions are understood to be interconnected rather than independent.
When any one of those variables is left to assumption or default, the failure may not appear immediately. It may show up in a production line that runs slower than expected, in a retail product that has started to open on the shelf, or in a transit claim that traces back to a collapsed corner. The cost of those failures is always higher than the cost of getting the specifications right before the first run begins.
For anyone responsible for specifying, sourcing, or managing folding carton packaging, the practical takeaway is straightforward: treat the tuck box as an engineered product, not a commodity item. The structural decisions behind it deserve the same level of scrutiny applied to any other component that carries a product through production, distribution, and into the hands of an end user.